Replacement Hydraulic Cylinders are often blamed when a machine moves unevenly, but trapped air is a more common cause. Air can enter through a low reservoir, a loose suction fitting, a damaged rod seal, an incorrectly filled cylinder, or turbulence in the hydraulic fluid. This guide explains how to bleed air from a hydraulic cylinder, identify the symptoms of air in a hydraulic system, and decide whether a hydraulic cylinder replacement is actually necessary. The key concepts are hydraulic system aeration, fluid compressibility, and hydraulic pump inlet conditions.
A cylinder containing oil should extend and retract in a controlled, repeatable motion. When air is present, the oil-air mixture acts like a spring. The cylinder may hesitate, bounce, drift, generate foam, or make a knocking sound. These symptoms can reduce positioning accuracy by several millimeters or create dangerous load movement, especially on lifting equipment. Before ordering Replacement Hydraulic Cylinders from Jiaheng or another supplier, confirm whether the problem is air, contamination, seal leakage, valve malfunction, or mechanical misalignment.
Air does not normally enter through a sound pressurized hydraulic line. It is usually pulled into the circuit at the pump inlet or introduced during maintenance. The following causes cover most field situations.
Why Air Enters Replacement Hydraulic Cylinders and Hydraulic Systems
If the reservoir level falls below the manufacturer’s minimum mark, the pump can draw air through the suction pipe. The pump then sends aerated fluid toward the directional valve and cylinder. A level that appears acceptable when the cylinder is retracted may become too low when the rod is extended because more oil is stored in the cylinder barrel.
Check the level with the machine in the position specified by the manufacturer. Do not simply fill the tank to the top. Hydraulic fluid expands with temperature, and an overfilled tank can force oil out through the breather or create pressure in the reservoir.
1. A low hydraulic-fluid level
The pump suction side can draw air without producing an obvious oil leak. A cracked hose, hardened O-ring, loose clamp, or damaged flange may allow air to enter while the negative pressure at the pump inlet prevents oil from escaping.
Inspect the entire suction path from the reservoir outlet to the pump inlet. Look for flattened hose sections, rubbing damage, wet fittings, and loose fasteners. A suction hose that is too small can also create excessive inlet vacuum and increase the chance of aeration and cavitation.
2. Loose or damaged pump suction connections
When a cylinder retracts, the rod seal is exposed to changing pressure. If the seal, gland, or rod surface is damaged, air can be pulled into the rod-side chamber during a rapid return stroke. The problem is more likely when the cylinder is mounted vertically, the rod is heavily loaded, or the return circuit creates a vacuum.
Oil around the rod is not proof that air is entering, but it is a useful warning. Check for a polished wear band, pitting, scoring, hardened seals, or side loading. If the rod is bent or the barrel is damaged, bleeding the cylinder will provide only temporary improvement; a seal repair or hydraulic cylinder replacement may be required.
3. A leaking rod seal or wiper seal
A new cylinder, rebuilt cylinder, hose, valve, or filter can contain a measurable volume of air. The risk increases when the cylinder is installed with the ports facing upward and the hoses are connected before the chamber is filled with oil.
Replacement Hydraulic Cylinders should be installed with clean capped ports, compatible seals, and the correct hydraulic fluid. Keep hose ends capped until connection. Even a small amount of dirt on a fitting can damage a valve spool or seal and create a second fault after the air has been removed.
4. Air introduced during cylinder installation or repair
Return oil entering above the fluid surface can create a vortex and carry air back toward the pump suction line. A missing baffle, damaged diffuser, or undersized reservoir can prevent air bubbles from separating before the oil is recirculated.
As a practical design check, the return outlet should generally remain below the fluid surface, and the suction and return ports should be separated by a baffle where possible. The exact reservoir size depends on duty cycle, heat generation, and manufacturer requirements; many mobile systems use a reservoir volume near one-half to one full pump flow per minute, but this is not a universal rule.
5. Turbulence and poor reservoir design
A clogged suction strainer, cold high-viscosity oil, undersized hose, or excessive pump speed can reduce inlet pressure. The resulting low-pressure condition may cause dissolved air to come out of solution. If the pressure falls low enough, the system can also experience cavitation, which produces a sharp rattling sound and damages pump surfaces.
Aeration and cavitation are related but not identical. Aeration means air is entering the oil. Cavitation occurs when local pressure falls below the fluid’s vapor pressure and vapor bubbles form and collapse. Both conditions can produce noise, vibration, heat, and inconsistent cylinder movement.
6. Excessive pump speed or restricted inlet flow
Air-related faults usually create a pattern rather than one isolated symptom. Record the machine temperature, oil level, load, pressure, and cylinder speed before disassembly.
- Jerky or spongy movement: the cylinder accelerates and slows as compressed air expands and contracts.
- Uneven extension or retraction: the cylinder may pause, then move suddenly after pressure builds.
- Foamy fluid: bubbles remain visible in the reservoir after the pump runs.
- Knocking or rattling: the pump or cylinder may produce a noise that changes with speed.
- Heat generation: aerated oil can increase internal friction and reduce volumetric efficiency.
- Load drift: a suspended load may move after the valve is centered, although drift can also result from valve leakage or worn piston seals.
- Slow cycle time: a cylinder may require 10 to 30 percent more time to complete a stroke, depending on the amount of entrained air and the load.
- Inaccurate positioning: the actuator may stop several millimeters away from the commanded position.
Do not diagnose air solely from a slow cylinder. A restricted return filter, worn pump, undersized valve, incorrect load-holding valve, bent rod, or contaminated fluid can produce similar results. A pressure gauge installed at the cylinder ports can separate a flow problem from a mechanical problem.
Symptoms of Air in a Hydraulic System Before You Replace a Cylinder
Bleeding is not a substitute for repairing the source of air entry. Find and correct the leak or design problem first. Prepare the following items:
- The machine service manual and hydraulic schematic
- The manufacturer-approved hydraulic fluid
- A clean transfer pump or sealed filling container
- Correct-size wrenches and a torque wrench
- Clean lint-free rags and an approved parts-cleaning solution
- A drain pan or transparent collection container
- Replacement O-rings, hose seals, or fittings if inspection identifies damage
- Pressure gauges rated above the maximum system pressure
- Safety glasses, gloves, protective footwear, and suitable protective clothing
- A rod support or mechanical blocking device for elevated equipment
Safety warning: Never loosen a hydraulic fitting while the circuit is pressurized. Hydraulic oil can penetrate skin at pressures above 100 bar, and injection injuries require immediate emergency treatment. Shut down the engine or motor, isolate electrical and hydraulic energy, lower the load, block moving parts mechanically, and verify zero pressure with the correct procedure before opening a line.
Required Preparation for Bleeding Air From a Hydraulic Cylinder
Step-by-Step Guide: How to Bleed Air From a Hydraulic Cylinder
Park the equipment on stable ground. Remove the load from the cylinder whenever possible. If the cylinder supports a boom, platform, bucket, or other elevated structure, install manufacturer-approved mechanical supports. Hydraulic pressure alone is not a safe support method.
For a double-acting cylinder, select a position that allows several slow full strokes without hitting a mechanical stop. For a single-acting cylinder, ensure the load cannot fall when the valve is operated.
Step 1: Place the machine in a safe bleeding position
Inspect the reservoir using the manufacturer’s level procedure. Add only the specified fluid through a clean filter or filling cart. Mixing fluids with different additive packages or viscosity grades can alter seal compatibility and air-release performance.
Take a small sample in a transparent container. Healthy oil should not contain a persistent layer of foam after standing. Milky oil may indicate water contamination, while dark particles or metallic glitter may indicate component wear. If the fluid is contaminated, bleeding alone will not restore reliable operation.
Step 2: Check the fluid level and condition
With the machine shut down, inspect suction hoses, clamps, flanges, O-rings, reservoir fittings, and the pump shaft seal. Tighten fasteners to the equipment manufacturer’s torque specification rather than guessing.
Inspect the return line for a loose diffuser or an outlet above the oil surface. Check that the suction strainer is not blocked. If the pump is noisy immediately after startup, stop the machine and investigate instead of repeatedly cycling the cylinder.
Step 3: Inspect the suction and return circuits
Start the system at the lowest permitted engine or motor speed. Allow the pump to circulate oil for approximately two to five minutes while observing the reservoir. Some manufacturers specify a longer warm-up period in cold conditions.
Listen for a high-pitched whine, rattling, or rhythmic knocking. Watch the reservoir for a vortex or continuous foam. If the oil level drops rapidly, shut down the pump and locate the cause before operating the cylinder.
Step 4: Start the pump at low speed and no load
Move the directional valve gradually so the cylinder extends at low speed. Stop approximately 50 to 100 mm before the mechanical end of stroke, then retract slowly. Repeat five to ten cycles, or follow the machine manufacturer’s specified number.
Do not slam the cylinder into its end stops. A hard stop can create a pressure spike and may damage the piston, gland, hose, or load-holding valve. Keep the load as low as possible during this stage.
Step 5: Cycle the cylinder slowly
Some cylinders include bleed screws at the highest points of the cap and rod ends. With the cylinder unloaded and pressure safely controlled, open the bleed point according to the manufacturer’s instructions. A typical sequence is:
- Place an approved collection hose over the bleed outlet.
- Open the bleed screw slightly, usually no more than one-quarter turn unless the manual specifies otherwise.
- Operate the cylinder at low speed.
- Allow air and foamy oil to escape until the flow becomes a continuous stream without bubbles.
- Close the bleed screw before changing direction or increasing speed.
- Repeat on the opposite chamber if the cylinder is double-acting.
Never place fingers near the outlet. Use cardboard or a shield to detect a leak, not a hand. Dispose of the collected oil according to local environmental requirements.
Step 6: Use the correct bleed points if provided
After cycling, the reservoir level may fall because the cylinder chambers have filled. Adjust the level to the specified mark. Inspect the return filter indicator and replace the filter if the restriction indicator is in the warning zone or if the service interval has been reached.
Do not use a filter with a micron rating or bypass setting that differs from the hydraulic design without approval. A filter that is too restrictive can create another inlet or return-flow problem.
Step 7: Recheck the reservoir and filter condition
Operate the cylinder at low, medium, and normal working speed. Record extension time, retraction time, pressure, noise, and temperature. A useful comparison is the time required to complete three identical cycles before and after bleeding.
If the movement remains smooth and the cycle time returns to the manufacturer’s specification, the air has probably been removed. If the cylinder becomes spongy again within minutes or hours, continue looking for an air-entry point rather than repeatedly bleeding it.
Step 8: Test the cylinder under controlled load
Field Case: A Hydraulic Cylinder That Was Replaced Too Early
A maintenance technician at a small material-handling workshop described a recurring problem with a double-acting lifting cylinder. After approximately 20 minutes of operation, the lift became jerky and stopped 5 to 8 mm above its normal position. The first assumption was a worn piston seal, so the team prepared to order a replacement cylinder.
The technician then checked the reservoir during a full extension cycle and found that the fluid level fell below the suction outlet. The machine had been topped up while the cylinder was retracted, and the level mark did not reflect the oil volume required during operation. The team corrected the fluid level, replaced a hardened suction-hose O-ring, and cycled the cylinder slowly eight times. The foam disappeared, the knocking stopped, and the measured stroke time returned from approximately 14 seconds to 10 seconds.
This case illustrates why a hydraulic cylinder replacement should not be the first response to unstable motion. The cylinder itself was serviceable; the fault was a combination of low reservoir level and suction-side air entry. The repair also reduced pump noise and prevented additional damage caused by aerated oil.
Common Errors When Bleeding Replacement Hydraulic Cylinders
Bleeding under full system pressure
Opening a bleed screw or hose under pressure can release oil at injection velocity. Use the manufacturer’s pressure-release procedure and verify pressure with a gauge where appropriate.
Using the wrong hydraulic fluid
Fluid viscosity affects pump inlet performance, leakage, heat, and cylinder speed. ISO VG 32 and ISO VG 46 oils are not interchangeable in every climate or machine. Follow the equipment manual and confirm the fluid’s operating-temperature range.
Filling through an unfiltered container
New oil is not necessarily clean enough for a precision hydraulic system. Use a clean transfer system with an appropriate filter. Particle contamination can damage proportional valves, piston pumps, and cylinder seals.
Running the cylinder rapidly at the end of stroke
Fast end-of-stroke impacts create pressure spikes and can force air into foam. Use low speed during initial bleeding and allow cushioning mechanisms to work correctly.
Replacing the cylinder without checking alignment
Side loading can damage a new cylinder in a short operating period. Check pin alignment, mounting brackets, bushings, rod straightness, and the load path. The rod should not be forced sideways to compensate for a misaligned structure.
Confusing aeration with cavitation
Persistent foam usually indicates aeration, while a sharp pump rattle under high demand may indicate cavitation. Both require investigation of the pump inlet, but the corrective actions may differ. Measure inlet vacuum if the manufacturer provides a permissible range.
Ignoring thermal expansion
Hydraulic oil expands as its temperature rises. Set the reservoir level at the specified temperature and machine position. Overfilling can cause leakage through the breather; underfilling can expose the suction inlet during operation.
When Is a Hydraulic Cylinder Replacement Necessary?
Bleeding is appropriate when the cylinder is structurally sound and the fault is caused by trapped air. Replacement or professional rebuilding is more appropriate when inspection finds:
- A bent rod or rod runout outside the manufacturer’s tolerance
- Deep rod pitting, scoring, or chrome damage
- A cracked barrel, gland, eye, flange, or mounting weld
- Persistent internal bypass across the piston seal
- Excessive rod play caused by worn guide bushings
- Repeated external leakage after correct seal installation
- Pressure loss that remains after the valve, pump, and hoses are confirmed operational
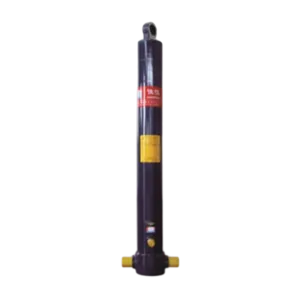
When selecting Replacement Hydraulic Cylinders, compare bore diameter, rod diameter, stroke, closed length, mounting style, port size, rated pressure, cushioning, seal material, and operating temperature. A cylinder with the correct stroke but an undersized rod may fail under buckling or side load. Jiaheng can help match these dimensions when the original part number is unavailable, but the working pressure and mounting geometry must be verified before ordering.
How to Prevent Air From Returning to the Hydraulic Cylinder
- Maintain the reservoir within the manufacturer’s operating range.
- Inspect suction hoses and fittings during scheduled service.
- Keep the return outlet below the oil surface where the design permits.
- Use the correct breather and replace it when blocked or saturated.
- Keep replacement cylinders and hoses capped until installation.
- Pre-fill large hydraulic components when the manufacturer permits it.
- Use clean oil and correctly rated filtration.
- Warm cold oil gradually instead of demanding full pump flow immediately after startup.
- Check rod alignment and avoid side loading.
- Record oil level, temperature, pressure, and cycle time during routine inspections.
Summary: Solving Air Problems in Replacement Hydraulic Cylinders
Air gets into a hydraulic cylinder mainly through low fluid level, suction-side leaks, damaged rod seals, poor reservoir design, maintenance work, or restricted pump inlet flow. The most reliable process is to make the machine safe, check the fluid and suction circuit, operate the cylinder slowly, bleed approved bleed points, restore the reservoir level, and test the system under a controlled load.
If the problem returns after bleeding, do not keep cycling the machine or immediately order Replacement Hydraulic Cylinders. Locate the air-entry source, inspect the pump and valves, and check cylinder alignment. A properly selected Jiaheng cylinder can restore reliable operation, but correct installation, clean hydraulic fluid, suitable seals, and adequate filtration determine how long the repair will last.
FAQ About Air in Hydraulic Cylinders
Can air enter a hydraulic cylinder when there is no visible oil leak?
Yes. A suction hose, pump inlet fitting, or rod seal can admit air while allowing little or no oil to escape. Negative pressure on the inlet side is often enough to pull air through a small gap.
How do I know whether the cylinder or pump is causing the problem?
Check the reservoir for foam and listen to the pump first. Then compare cylinder pressure and movement in both directions. If several actuators are noisy or unstable, investigate the pump, reservoir, and common supply circuit. If only one cylinder is affected, inspect its seals, ports, alignment, and internal bypass.
Can trapped air damage a hydraulic cylinder?
Yes. Compressed air can cause impact loading, unstable motion, seal extrusion, excessive heat, and pressure fluctuations. Aerated oil can also reduce pump lubrication and shorten component life.
How many cycles are needed to remove air?
There is no universal number. Five to ten slow full cycles often removes air from a correctly installed cylinder, but large cylinders, long hoses, and systems without bleed points may require more. Stop if the oil foams, the pump becomes noisy, or the load moves unpredictably.
Should I replace the hydraulic fluid after bleeding?
Replace or filter the fluid if it is visibly foamy for an extended period, contaminated with water or particles, overheated, or outside the specified service interval. If the oil is clean and the air-entry cause is corrected, a complete fluid change may not be necessary.
Can I bleed a cylinder by loosening the hydraulic hose?
Only if the machine manufacturer specifically permits that procedure and the circuit has been isolated and depressurized. A hose connection is not a substitute for a designed bleed point. Improper loosening can cause injury, contamination, and uncontrolled actuator movement.
When should I contact a hydraulic-cylinder manufacturer such as Jiaheng?
Contact a qualified manufacturer when the rod is damaged, the cylinder leaks after resealing, the mounting dimensions are unclear, the original cylinder is obsolete, or the operating pressure and load require a new design. Provide bore, rod diameter, stroke, mounting dimensions, port details, working pressure, speed, fluid type, and photographs of the existing assembly.